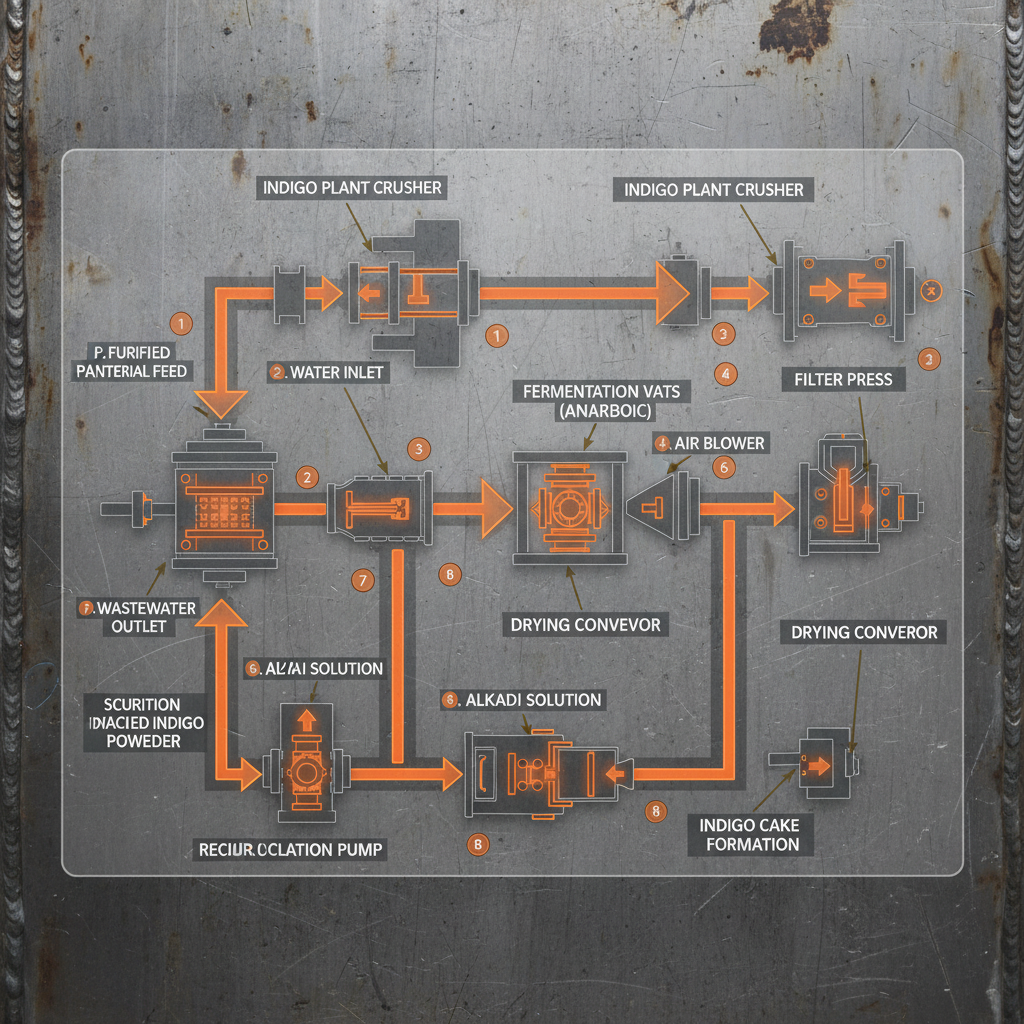
The global textile industry relies heavily on a diverse palette of pigments, where the pursuit of the perfect dark shade has led to significant advancements in chemical synthesis. While traditional methods have laid the groundwork, modern indigo dye production has evolved to integrate higher precision and stability, ensuring that fabrics meet the rigorous demands of contemporary fashion and industrial utility.
Understanding the nuances of color chemistry is essential for manufacturers who aim to balance aesthetic depth with material longevity. The challenge lies in achieving a saturated, deep black or blue that resists fading and maintains consistency across large batches of denim and blended fabrics, a goal that requires strict adherence to quality standards and cutting-edge formulation techniques.
By optimizing the processes involved in indigo dye production, the industry can now offer high-performance solutions like Sulphur Black, which provides the intensity and durability required for professional-grade garments. This evolution ensures that every fiber is saturated, providing a sophisticated look that meets both consumer expectations and environmental regulations.
Global Relevance of Indigo Dye Production
The global demand for deep-toned textiles, particularly in the denim sector, has placed indigo dye production at the center of textile chemical engineering. With the rise of fast fashion and sustainable luxury, the ability to produce consistent, vibrant black and blue shades is no longer just a preference but a market necessity.
Industry standards now dictate a move toward dyes that offer superior penetration and coverage. By utilizing high-quality ingredients and cutting-edge technology, manufacturers can ensure that pigments adhere firmly to cotton, hemp, and viscose fibers, reducing waste and enhancing the overall lifecycle of the garment.
Defining Modern Dyeing Standards
In simple terms, modern dyeing processes involve the chemical synthesis of pigments that can bond effectively with various fiber types. This process is not merely about color but about the chemical interaction between the dye molecule and the textile substrate, ensuring that the final product is resistant to washing and abrasion.
For products like Sulphur Black, the standard is defined by "Bright Black Flaky Granules" with strength levels ranging from 180% to 240%. This precision in strength and shade—whether greenish or reddish—allows brands to maintain strict visual identity across different production lines globally.
Beyond the color, modern standards emphasize safety and regulatory compliance. Ensuring that dyes are free from harmful substances is a critical component of the production chain, meeting the highest industry benchmarks to protect both the end consumer and the environment.
Core Components of High-Performance Dyes
The efficacy of any colorant depends on its chemical purity and physical form. In the context of indigo dye production and its derivatives, the moisture content (kept ≤6%) and insoluble matters (kept ≤0.3%) are key indicators of quality that prevent clumping and ensure an even distribution of color.
Saturation and depth are achieved through the correct strength percentage. By offering customized strengths of 180, 200, 220, and 240, manufacturers can provide a scalable solution that adapts to the specific absorption rates of different fabrics, such as cotton-blended materials or pure viscose fibers.
Another core component is the shade customization. Whether a client requires a greenish or reddish undertone, the ability to pivot the chemical composition allows for a wider range of aesthetic expressions within the black and indigo spectrum, enhancing the versatility of the final textile product.
Practical Applications in Denim and Textiles
The most prominent application of these high-grade dyes is in the creation of premium denim. Sulphur Black is specifically formulated to deliver a deep, rich color that penetrates every thread, ensuring that the dark, sophisticated look craved by denim enthusiasts is achieved consistently.
Beyond denim, these dyes are instrumental in processing cotton and dimension/cotton blended fabrics. The versatility extends to hemp and viscose fibers, where the dye's excellent coverage ensures that even coarse or highly absorbent fibers achieve a uniform and intense black hue without streaking.
Comparison of Indigo Dye Production Performance Metrics
Long-Term Value of Color Stability
The true value of a professional dyeing process lies in its longevity. For the end-user, this means garments that retain their intense black color even after multiple washes, avoiding the premature fading that often plagues lower-quality textiles. This reliability builds trust between the brand and the consumer.
From a business perspective, utilizing a cost-effective yet high-performance solution reduces the need for re-dyeing and minimizes product returns. By ensuring that the color does not wash out easily, manufacturers can position their products in the premium segment of the market, emphasizing durability and quality.
Future Trends in Chemical Coloration
The future of indigo dye production is leaning heavily toward the intersection of automation and sustainability. Digital transformation in the mixing process allows for near-perfect shade reproduction, eliminating the guesswork and reducing chemical waste during the calibration phase.
Moreover, there is a growing trend toward "green chemistry," where the focus is on reducing the environmental footprint of the production cycle. This includes developing dyes that require less water for rinsing and utilizing ingredients that are biodegradable without compromising the depth of the black shade.
Innovation is also steering toward smart textiles, where dyes may eventually incorporate functional properties, such as UV protection or thermal regulation, all while maintaining the classic, deep aesthetic of traditional sulphur and indigo dyes.
Overcoming Challenges in Dye Application
One of the most common challenges in the industry is achieving uniform penetration on blended fabrics. Because cotton and synthetic fibers absorb dyes differently, "streaking" can occur. The solution lies in the meticulous selection of dye strength and the use of cutting-edge application technology to ensure total saturation.
Storage and handling also present significant hurdles. Dyes must be kept in dry conditions with adequate ventilation, avoiding direct sunlight and dampness to prevent degradation. Proper packaging in 20kg cartons or 25kg PP woven bags is essential to maintain the validity of the product for its two-year shelf life.
Finally, the conflict between intensity and softness is a constant struggle. By optimizing the rinsing process and using high-purity granules, manufacturers can achieve a deep black that doesn't make the fabric feel stiff, ensuring that the final garment is as comfortable as it is visually striking.
Core Analysis of Dye Application and Storage Standards
| Fabric Type |
Recommended Strength |
Saturation Level |
Durability Score |
| Pure Cotton |
220% - 240% |
High |
9.5 |
| Cotton Blend |
200% - 220% |
Medium-High |
8.8 |
| Hemp Fiber |
240% |
High |
9.2 |
| Viscose |
180% - 200% |
Medium |
8.0 |
| Denim Twill |
220% |
Very High |
9.8 |
| Linen Mix |
200% |
Medium |
8.5 |
FAQS
The strength percentage (e.g., 180% to 240%) refers to the concentration of the active pigment. A higher strength allows for a deeper, more intense black or blue shade using less total product. This is crucial for achieving the "rich black" look in denim without over-saturating the fabric to the point of stiffness.
Our current Sulphur Black and indigo-based products are optimized for natural fibers and blends, specifically cotton, hemp, and viscose. For 100% synthetic fibers like polyester, different chemical bonding agents (disperse dyes) are typically required, as the molecular structure of polyester does not react the same way as cellulose-based fibers.
The "shade" refers to the subtle undertone of the black color. A greenish shade provides a cooler, more metallic appearance, while a reddish shade offers a warmer, deeper tone. These customizations allow designers to match specific seasonal palettes or brand guidelines while maintaining a professional black finish.
To maintain the integrity of the dye, it must be stored in a cool, dry area with adequate ventilation. It is critical to avoid direct sunlight (UV exposure) and damp environments, as moisture can lead to clumping and degradation of the pigment strength, potentially shortening the shelf life.
Yes, our dyes undergo rigorous testing to ensure they meet the highest industry standards and comply with international regulations regarding harmful substances. Once the dyeing and rinsing process is complete, the final textile is safe for consumer use and compliant with safety certifications.
We provide standard 20kg cartons and 25kg PP woven bags. However, we are fully capable of customizing packaging based on the customer's specific logistical requirements to ensure safe transport and easy handling during the industrial dyeing process.
Conclusion
The mastery of indigo dye production and the application of specialized products like Sulphur Black represents the perfect synergy of chemistry and art. By focusing on key parameters—such as strength, moisture control, and shade precision—manufacturers can produce textiles that are not only visually stunning but also durable and safe. The ability to deliver a deep, saturated black across various fibers ensures that the final product stands out in a competitive global market.
As the industry moves toward a more sustainable and digitally integrated future, the emphasis will remain on quality and consistency. We encourage textile producers to prioritize high-purity pigments and rigorous storage standards to maximize the lifespan of their products. For those looking to elevate their denim game with professional-grade colorants, exploring cutting-edge dyeing solutions is the first step toward market leadership. Visit our website: www.wuxin-group.com