The global textile industry relies heavily on specialized coloring agents to meet the aesthetic demands of the modern consumer, with the pursuit of the perfect denim shade remaining a top priority for manufacturers. Among these, the application of high-purity pigments is essential for achieving the deep, characteristic hues that define quality apparel. Understanding the chemical properties and application methods of these agents is key to optimizing production efficiency and product longevity.
In the competitive landscape of apparel manufacturing, the choice of coloring materials directly impacts the final garment's value, particularly regarding color fastness and the ability to undergo specialized finishing processes. As global demand for sustainable and high-performance textiles grows, the industry is shifting toward more precise purity standards to reduce waste and ensure consistency across massive production batches.
For professionals in the chemical and textile sectors, sourcing a premium indigo blue dye for jeans is not merely a procurement task but a strategic decision that influences the feasibility of stone washing and acid washing effects. By utilizing a product with a purity level of ≥94%, manufacturers can ensure that the crystalline structure of the dye interacts optimally with cotton fibers to produce the iconic denim look.
Chemical Composition and Physical Properties of Indigo
Indigo is a dark blue crystalline powder characterized by its specific chemical formula, C16H10N2O2. One of its most distinctive physical properties is its sublimation point, occurring between 390–392 °C (734–738 °F), which indicates a high level of thermal stability under standard processing conditions.
From a solubility perspective, this substance is insoluble in water, alcohol, or ether, which is precisely what makes it ideal for specific textile applications. However, it can be dissolved in concentrated sulfuric acid, nitrobenzene, chloroform, and DMSO, allowing chemists to manipulate its state for various industrial processes.
Industrial Application in Denim Production
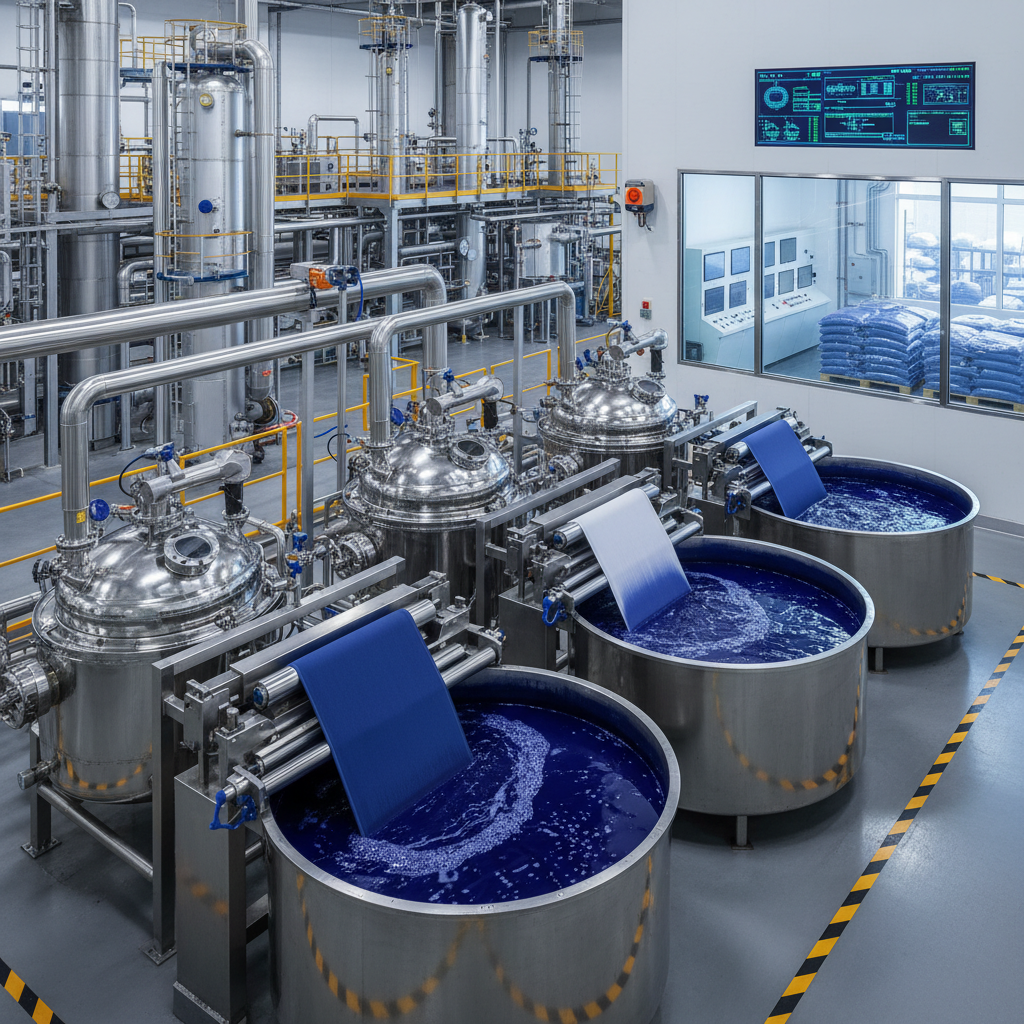
The primary industrial utility of this pigment is the dyeing of cotton yarn, which serves as the foundational step in the manufacturing of denim cloth. Because of its unique affinity for cotton, it is the definitive indigo blue dye for jeans, ensuring that the fabric maintains the depth of color required by global fashion brands.
Beyond denim, the dye is utilized in smaller quantities for the treatment of wool and silk fabrics. While the scale of application is lower compared to cotton, the versatility of the crystalline powder allows for a range of blue shades depending on the concentration and the substrate used.
The industrial appeal lies in the way the dye sits on the fiber. Unlike some pigments that penetrate deeply and permanently, indigo allows for the strategic removal of color through mechanical or chemical means, which is the basis for all modern denim aesthetics.
Technical Quality Standards for High-Purity Dye
To ensure consistency in large-scale textile batches, strict quality standards must be maintained. A professional-grade indigo blue dye for jeans should feature an appearance of dark blue even grains, indicating a uniform particle size distribution that prevents streaking during the dyeing process.
The purity level is a critical metric, with industry standards requiring a purity of ≥94%. Furthermore, the water content must be kept ≤1% and iron ion content limited to ≤200ppm. These constraints are vital because impurities can lead to unpredictable color shifts or compromise the structural integrity of the cotton yarn.
Adherence to these technical specifications ensures that the dye performs predictably during the sublimation and dissolution phases. By controlling these parameters, manufacturers can reduce the amount of wasted fabric and lower the overall cost of production while maintaining a premium end product.
Efficiency Analysis of Dye Consumption
One of the most surprising aspects of denim production is the efficiency of the coloring process. On average, a single pair of blue jeans requires only between 3 grams (0.11 oz) and 12 grams (0.42 oz) of dye, depending on the desired depth of the shade and the weight of the denim cloth.
This low consumption rate makes the high-purity crystalline powder an economically viable solution for mass production. When scaled to millions of units, the precision of the dye's purity ensures that these small quantities yield consistent results across different manufacturing facilities.
Efficiency Rating of Different Indigo Application Methods
Specialized Finishing and Washing Effects
The unique chemical property of indigo is that it does not fully penetrate the cotton fiber, leaving the core of the yarn white. This characteristic is what enables the creation of high-value fashion effects, such as stone washing and acid washing, which can be applied quickly to create a worn-in, vintage look.
Because the indigo blue dye for jeans is designed to be slightly unstable under abrasive conditions, it allows designers to create complex gradients and fades. This versatility makes it an irreplaceable component in the denim industry, as other dyes would simply remain static and resist these aesthetic modifications.
Safe Transportation and Industrial Logistics
Transporting high-purity indigo requires strict adherence to safety protocols to prevent contamination and degradation. It is strictly prohibited to mix or transport this dye with oxidants or edible chemicals, as such interactions could lead to chemical instability or hazardous reactions.
Environmental protection is equally critical during transit. The product must be shielded from direct sun exposure, rain, and high temperatures. When shipments are stopping over, they must be kept far away from fire, heat sources, and any high-temperature industrial areas to maintain the crystalline structure.
Logistics options are flexible to meet customer needs, ranging from 20kg cartons to 500-550kg bulk bags. Whether shipping in 20’GP or 40’HQ containers, the priority remains the prevention of moisture ingress and the avoidance of heat-induced oxidation.
Optimized Storage and Stability Management
To maintain a validity period of two years, indigo must be stored in a cool, ventilated, and dry warehouse. The temperature must be strictly controlled below 25 degrees Celsius, and the relative humidity must remain below 75% to prevent the powder from clumping or deteriorating.
Sealing is the most critical factor during the rainy season. The packaging must be completely airtight because long-term exposure to air or sunlight leads to oxidation, which destroys the color purity and effectiveness of the dye.
Furthermore, it is mandatory to store the dye in isolation from acids, alkalis, reducing agents, and strong oxidants like potassium nitrate or ammonium nitrate. This isolation prevents accidental combustion or chemical deterioration, ensuring the product remains in peak condition for production.
Summary of Indigo Storage and Handling Requirements
| Control Dimension |
Required Specification |
Risk of Non-Compliance |
Management Priority |
| Temperature |
Below 25°C |
Thermal Decomposition |
High |
| Humidity |
Below 75% RH |
Moisture Clumping |
Medium |
| Air Exposure |
Completely Sealed |
Oxidative Deterioration |
Critical |
| Chemical Isolation |
Away from Oxidants/Acids |
Combustion Risk |
Critical |
| Light Exposure |
Dark Storage |
Photo-oxidation |
Medium |
| Transport Safety |
No Mixed Edibles |
Contamination |
High |
FAQS
For industrial-grade denim production, a purity of ≥94% is the gold standard. This high level of purity ensures that the dark blue crystalline powder provides a consistent shade and responds predictably to chemical reduction and oxidation processes. Lower purity dyes may contain impurities that cause uneven coloring or interfere with the fabric's ability to be stone-washed.
Depending on the desired shade and denim weight, a typical pair of blue jeans requires between 3 grams (0.11 oz) and 12 grams (0.42 oz) of dye. Because the pigment is highly concentrated and efficient, a small amount of high-purity crystalline powder is sufficient to color the cotton yarn effectively.
Indigo's water insolubility is a key feature that allows it to sit on the surface of the fiber rather than penetrating it completely. To apply it, the dye must be dissolved in specific solvents or chemically reduced to a soluble form (leuco-indigo) before being applied to the yarn and then oxidized back to its insoluble blue state via air exposure.
The primary risks are oxidation and moisture. If exposed to air or sunlight for extended periods, indigo will oxidize and deteriorate. Additionally, humidity above 75% can cause the powder to clump. It must be stored below 25°C and kept isolated from strong oxidants, acids, and alkalis to prevent combustion or chemical breakdown.
Yes, while its primary use is for cotton yarn in denim production, indigo is also used in smaller quantities for dyeing wool and silk. However, the application techniques differ slightly due to the protein-based nature of these fibers compared to the cellulose-based nature of cotton.
Transport requires strict environmental controls. It must be protected from rain and sun, and kept away from high-temperature areas. It is strictly forbidden to transport indigo with edible chemicals or oxidants. Packaging ranges from 20kg cartons to 500kg bags to ensure the material remains sealed and stable during transit.
Conclusion
The technical precision of indigo production—from maintaining a purity of ≥94% to controlling iron ion content—is what enables the global denim industry to produce consistent, high-quality apparel. By understanding the chemical properties of C16H10N2O2 and strictly adhering to storage and transport protocols, manufacturers can maximize the efficiency of dye consumption while achieving the sophisticated washing effects that define modern fashion.
As the industry moves toward more sustainable practices, the reliance on high-stability, high-purity agents will only increase to minimize chemical waste. For companies looking to optimize their denim production line, investing in a premium indigo blue dye for jeans is the most effective way to ensure product longevity and aesthetic excellence. Visit our website: www.wuxin-group.com