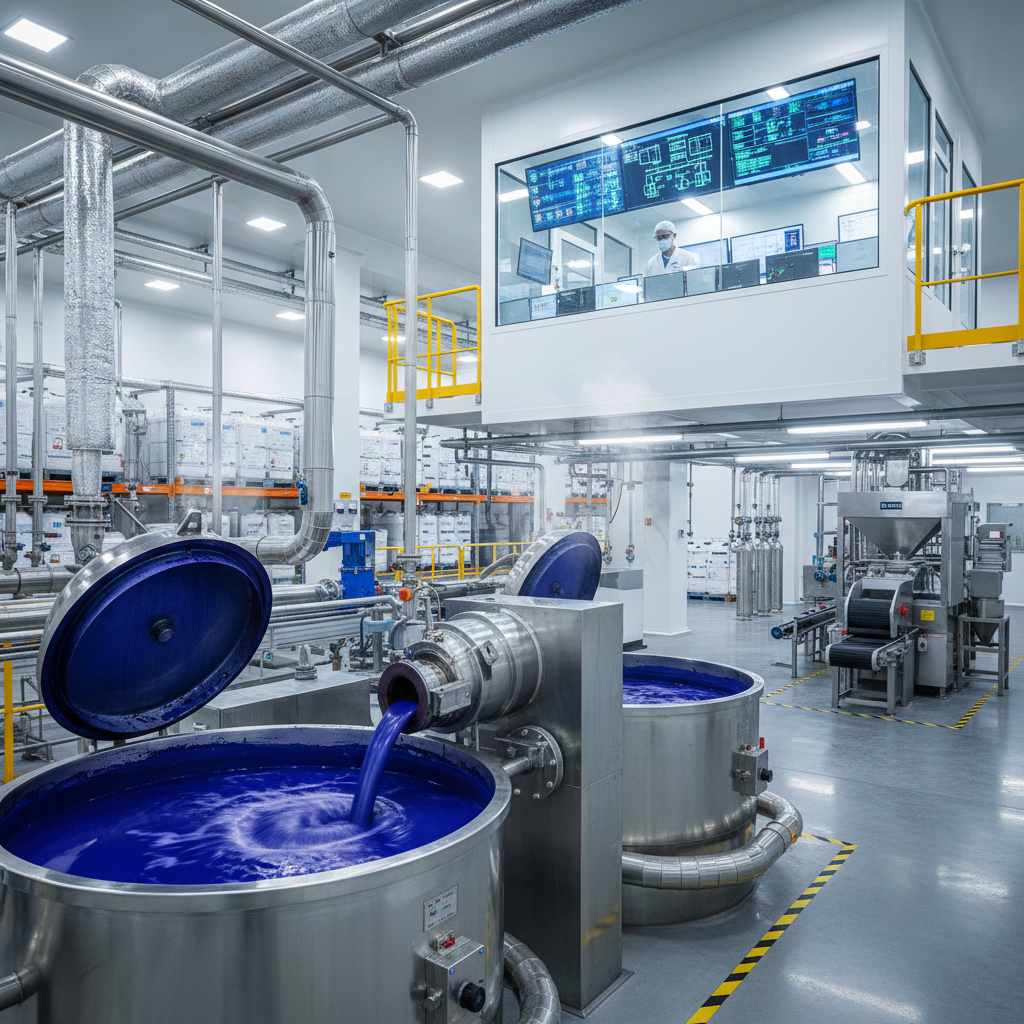
The textile industry has always been driven by the pursuit of deep, enduring color, and while many look toward various pigments, the demand for high-performance dyes remains a global priority. Achieving a professional finish on denim and cotton fabrics requires a sophisticated understanding of chemical penetration and color fastness, ensuring that the aesthetic appeal lasts through years of wear.
In the modern manufacturing landscape, the challenge lies in balancing intense saturation with cost-efficiency and regulatory compliance. Many producers struggle with dyes that fade prematurely or fail to penetrate the core of the fiber, leading to inconsistent batches and dissatisfied end-consumers in the competitive global apparel market.
To solve these challenges, industry professionals often turn to specialized solutions like indigo blue fabric dye and high-strength sulphur blacks to achieve that sought-after, sophisticated depth. By utilizing cutting-edge chemical formulations, manufacturers can now ensure their textiles meet the highest international standards for longevity and vibrancy.
Global Relevance of Professional Fabric Dyeing
The global textile market relies heavily on the precision of chemical dyeing to maintain brand consistency and consumer trust. Whether it is the deep obsidian of high-end denim or the classic hues achieved via indigo blue fabric dye, the ability to produce saturated, wash-resistant colors is a critical competitive advantage for manufacturers across Asia and Europe.
Modern standards, such as those aligned with ISO certifications, demand that dyes not only provide aesthetic value but also adhere to strict safety regulations regarding harmful substances. This shift toward "cleaner" chemistry ensures that high-performance dyes can be exported globally without facing regulatory hurdles.
Technical Definition and Industrial Meaning
In industrial terms, high-performance fabric dyeing refers to the application of chemical agents that create a permanent molecular bond with the fiber. While many refer to the process through the lens of indigo blue fabric dye, the broader category includes sulphur-based dyes designed for intense saturation and coverage.
These dyes are typically characterized by their physical form—such as bright black flaky granules—and their chemical strength, often measured in percentages (e.g., 180%, 200%, or 240%). This strength determines the amount of dye required to achieve a specific shade, directly impacting the production cost and efficiency of the textile mill.
Ultimately, the industrial meaning of these dyes extends beyond simple color; it is about "coverage" and "penetration." A superior dye ensures that every thread of a cotton or viscose blend is saturated, preventing the "frosting" or uneven fading that often plagues low-quality textiles.
Core Components for Superior Color Depth
Achieving professional depth starts with the selection of the right chemical grade. For those utilizing indigo blue fabric dye or sulphur black, the moisture content must be kept low (typically ≤6%) to ensure stability and prevent clumping during the mixing process.
Another critical factor is the shade customization. Industrial dyes are rarely "one size fits all"; they are often adjusted to be greenish or reddish to complement the base fabric. This allows manufacturers to fine-tune the final look of the garment, ensuring that the indigo blue fabric dye effect is harmonized with the desired fashion trend.
Finally, the purity of the product—measured by insoluble matters (≤0.3%)—is what separates professional grade dyes from amateur ones. High purity means fewer streaks in the fabric and a more uniform application, which is essential for high-volume denim production.
Practical Applications in Global Textiles
The most prominent application of these high-strength dyes is in the denim industry, where a deep, rich black or a classic indigo blue fabric dye appearance is non-negotiable. These dyes are primarily used for cotton, cotton-blended fabrics, hemp, and viscose fibers, making them versatile for everything from luxury apparel to industrial workwear.
In remote industrial zones and large-scale manufacturing hubs, the ease of application is just as important as the color itself. By using a simplified application process, factories can rapidly switch between shades—such as greenish-black or reddish-black—to meet the shifting demands of global fashion cycles.
Efficiency Rating of Various Dyeing Methods
Long-Term Value and Reliability
The true value of a professional dye lies in its longevity. When using high-quality indigo blue fabric dye or sulphur black, the result is a textile that retains its intense color even after multiple rigorous washes. This reliability reduces the rate of product returns and enhances the brand's reputation for quality.
Furthermore, the cost-effectiveness of high-strength granules (180%-240%) means that less product is needed to achieve the desired saturation. This reduction in raw material usage, combined with a low failure rate in the dyeing vat, provides a significant financial advantage for large-scale producers.
Future Trends in Dyeing Technology
The future of the industry is leaning heavily toward sustainability and digital precision. We are seeing a transition where the application of indigo blue fabric dye is being integrated with automated dosing systems to eliminate human error and reduce chemical waste.
Additionally, there is a growing emphasis on "Green Chemistry." New formulations are being developed to ensure that high-intensity colors can be achieved with lower water consumption and less environmental impact, aligning with global ESG (Environmental, Social, and Governance) goals.
Automation and AI-driven color matching are also becoming standard, allowing manufacturers to replicate a specific shade of indigo blue fabric dye across different batches with 99.9% accuracy, regardless of the fabric source.
Overcoming Industrial Dyeing Challenges
One of the most common challenges in the field is "color bleeding" or uneven saturation. By ensuring the use of dyes with insoluble matters ≤0.3% and utilizing the correct temperature controls, manufacturers can overcome these hurdles and produce textiles that are perfectly uniform.
Another issue is storage degradation. To maintain the potency of indigo blue fabric dye and other sulphur dyes, it is imperative to store them in dry, well-ventilated areas away from sunlight and dampness. This prevents the oxidation that can alter the shade before the dye even hits the fabric.
For those struggling with cost, the solution is moving toward high-strength concentrates. By switching to 220% or 240% strength granules, the cost per unit of "deepness" decreases, allowing for a more sophisticated look without inflating the production budget.
Technical Specifications and Performance Analysis of Industrial Dyes
| Dye Variant |
Strength Grade |
Saturation Score |
Wash Fastness |
| Sulphur Black (Greenish) |
200% |
9.5 |
High |
| Sulphur Black (Reddish) |
220% |
9.8 |
High |
| Indigo Blue Grade A |
180% |
8.7 |
Medium-High |
| Indigo Blue Premium |
240% |
9.9 |
Very High |
| Cotton Blend Special |
200% |
9.0 |
High |
| Viscose Variant |
180% |
8.5 |
Medium |
FAQS
To prevent fading, it is crucial to use high-strength dyes with a low percentage of insoluble matters. Ensuring proper penetration into the fiber during the dyeing process and following strict wash-fastness protocols will guarantee that the color remains intense over time.
Yes, these professional dyes are specifically formulated for cotton and cotton-blended fabrics. They are also highly effective for dyeing hemp and viscose fibers, providing a consistent and rich color across different material compositions.
Strength percentage refers to the concentration of the active coloring agent. A higher percentage (like 240%) means the dye is more concentrated, allowing you to achieve the same deep shade using less physical product, which improves cost-efficiency.
Dyes should be stored in a cool, dry environment with adequate ventilation. It is critical to avoid direct sunlight and damp conditions, as moisture and UV exposure can degrade the chemical stability and alter the final shade.
Yes, our professional dyes undergo rigorous testing to meet industry standards and comply with regulations regarding harmful substances, ensuring they are safe for both the workers and the end consumers.
These are subtle undertones added to the dye to help manufacturers achieve a specific aesthetic. Greenish shades provide a cooler, crisper tone, while reddish shades offer a warmer, deeper look, allowing for precise customization of the final textile.
Conclusion
In summary, the success of high-end textile production depends on the precision, strength, and purity of the dyes used. Whether utilizing sulphur black or indigo blue fabric dye, the focus must remain on achieving deep saturation and long-term wash-fastness through the use of high-strength granules and strict quality control.
As the industry moves toward a more sustainable and automated future, the adoption of high-purity, compliant chemicals will be the key to maintaining a competitive edge. We encourage manufacturers to prioritize technical specifications over low-cost alternatives to ensure the longevity and dignity of their final products. Visit our website: www.wuxin-group.com